Pulley Runout and Concentricity: What to Specify should be approached as a drive-system decision. The useful starting point is the mating belt and machine interface, followed by tooth count, working width, shaft mounting and duty conditions. This guide explains the checks that help an engineer or buyer turn timing pulley runout concentricity into an RFQ that can be verified against a catalogue row or drawing.
Establish the Drive Identity for Pulley Runout and Concentricity
For timing pulley runout concentricity, identify the complete belt marking before comparing pulley diameters. HTD is a curvilinear synchronous system and the nominal pitch must stay associated with its profile family. Record the driver and driven tooth counts when an existing ratio must be preserved. For a new drive, document the target speed ratio, driver speed and expected load before choosing tooth counts. This prevents a component-level decision from overriding the machine requirement.
For a replacement project, compare the measured value with the installed belt and machine arrangement before deciding that a catalogue row is equivalent. For a new project, document the design basis so later maintenance teams can understand why the pitch, tooth count and mounting style were selected.
Dimensions That Control Pulley Runout and Concentricity
A pulley can match pitch and tooth count yet still fail to fit the machine because the bore, hub, flange or axial position differs. Measure the shaft interface, belt-face width, hub projection on both sides and the belt line relative to a stable machine datum. Where a taper bush is used, record both the pulley series and bush code. Where a finished bore is required, include fit, keyway and any retaining method on the drawing.
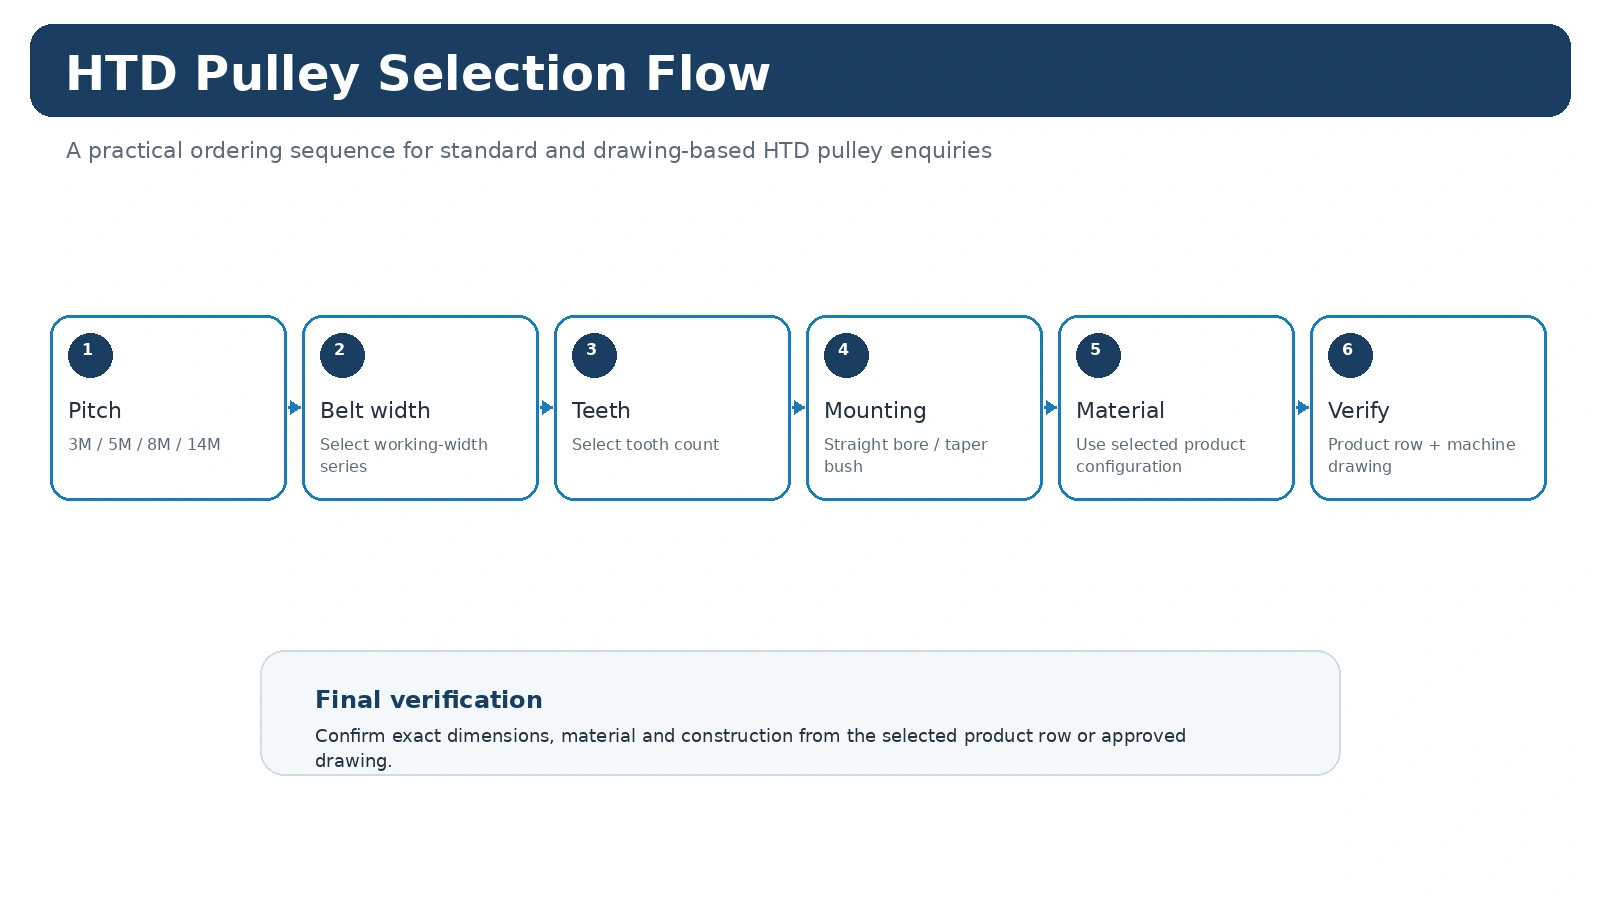
For a replacement project, compare the measured value with the installed belt and machine arrangement before deciding that a catalogue row is equivalent. For a new project, document the design basis so later maintenance teams can understand why the pitch, tooth count and mounting style were selected.
Put Pulley Runout and Concentricity in the Real Machine Context
The same nominal timing pulley runout concentricity component can see very different service depending on the machine. Starts per hour, reversing, shock loading, continuous operating time, temperature, contamination, cleaning and access for tensioning all influence the drive. A compact automation axis emphasizes repeatable motion and controlled alignment, while a conveyor or process machine may emphasize continuous duty and service access. Supply these conditions instead of asking the pulley to be selected from size alone.
For a replacement project, compare the measured value with the installed belt and machine arrangement before deciding that a catalogue row is equivalent. For a new project, document the design basis so later maintenance teams can understand why the pitch, tooth count and mounting style were selected.
Inspection Points for Pulley Runout and Concentricity
Inspection should focus on dimensions that affect the drive: the shaft interface, axial location, tooth condition, face width and any drawing-controlled runout or datum relationship. A generic quality statement does not define acceptance. If a dimensional report, material document or order-specific record is required, identify it before production. During maintenance, watch for flange damage, edge wear, debris and signs that the pulley has moved on the shaft.
For a replacement project, compare the measured value with the installed belt and machine arrangement before deciding that a catalogue row is equivalent. For a new project, document the design basis so later maintenance teams can understand why the pitch, tooth count and mounting style were selected.
Questions to Resolve Before Selecting Pulley Runout and Concentricity
What exact HTD profile and width is installed or specified?
What ratio or existing tooth count must be preserved?
What bore, fit, keyway or taper-bush arrangement is required?
How much hub projection and flange clearance is available?
What are the speed, load, starts, reversing and operating hours?
Which drawing, material or inspection records must accompany supply?
Drawing and Datum Strategy
When runout or concentricity matters, state the feature and datum relationship being controlled. A tolerance with no datum can be ambiguous. For repeat supply, keep the approved drawing revision and inspection requirement connected to the product identifier.
Record the conclusion in the RFQ or drawing so the same decision is visible to engineering, purchasing and inspection.
What to Send With the RFQ
Send profile, tooth count, belt width, shaft interface, hub/flange details, quantity, destination and a drawing or replacement measurement sketch. Add speed, ratio, load, center distance and environment for a new drive. Review the ایچ ٹی ڈی پروڈکٹ فیملیز، استعمال کریں۔ انتخاب گائیڈ, or compare the relevant application notes.
Specify Runout Only Where the Application Requires It
Do not publish one universal runout value for every HTD pulley. If the application has a functional limit, put the datum, measured feature and acceptable limit on the drawing or inspection requirement.
Keep measured values, catalogue references and project requirements clearly separated. If a required point is not stated in the relevant catalogue table or approved drawing, include it as an RFQ question or drawing requirement instead of filling the gap with a plausible but unverified value.
Measurement Method Matters
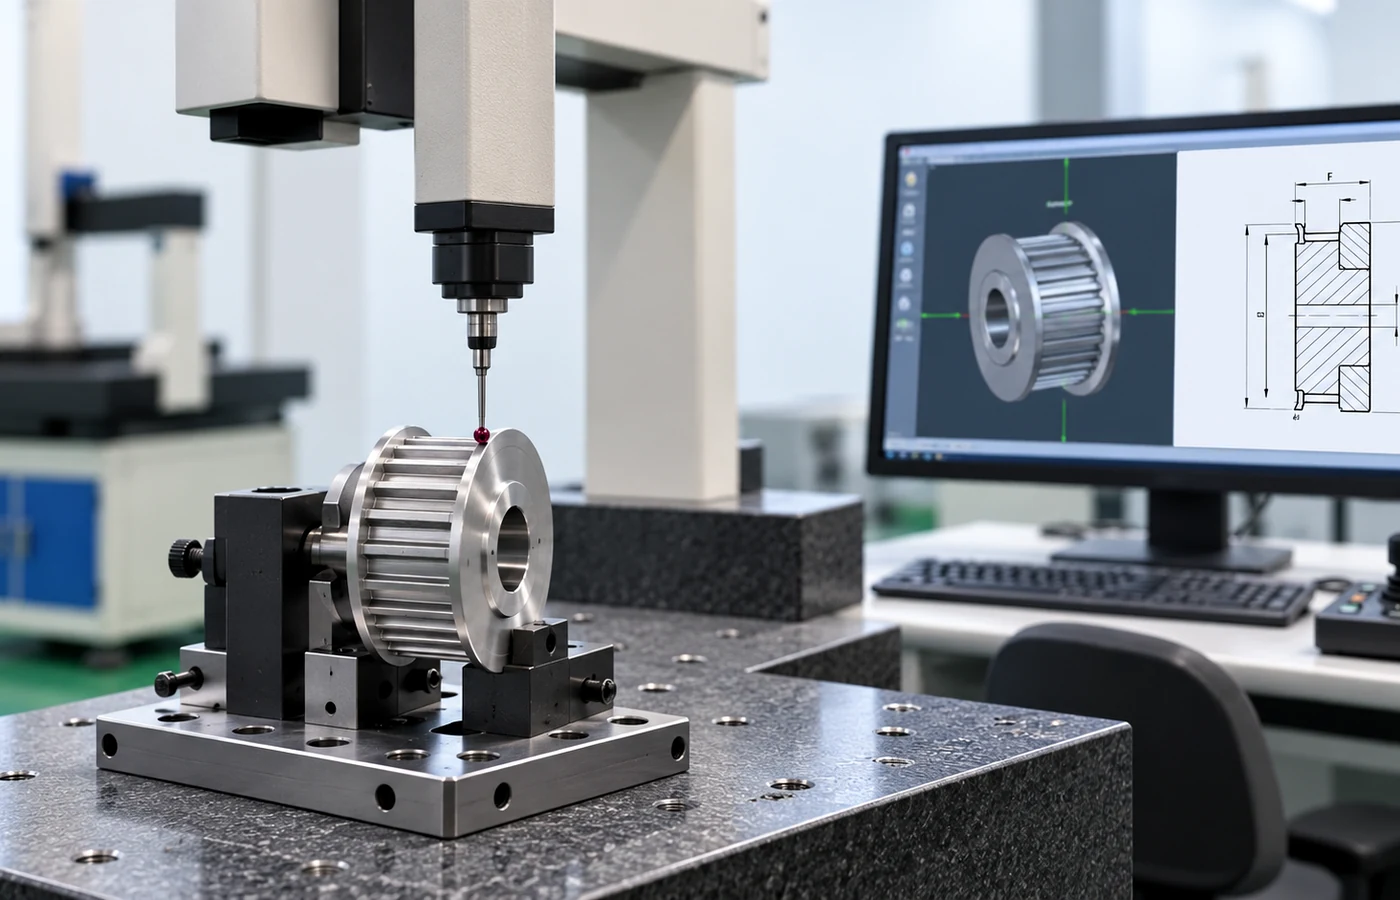
A runout result depends on how the part is mounted and what surface is referenced. Define the inspection setup when the value is critical so supplier and buyer are checking the same condition.
The purchasing record should keep a clear link between the machine requirement and the selected pulley. That means the complete belt or profile identity, tooth count, working width and shaft-interface information remain together with the product code. Any special material, finish, controlled tolerance, marking or report requirement should be stated separately so it cannot be mistaken for a universal feature of the whole family.
Procurement and Documentation
Once the selection is clear, keep the accepted product identity, quantity, destination and drawing revision on the same purchase line. Standard catalogue parts are normally planned around production-quantity minimums, while larger or higher-value items can be reviewed against the practical order value. Qualified new-client samples of 1–5 pieces may be reviewed at sample pricing when the configuration and manufacturing route are suitable.
Mixed-model orders can be consolidated toward a practical order value of about USD 1,500. Special materials and special processes follow the minimum quantity required by that process. Very small one- or two-piece requests are handled only as qualified engineering validation or paid-sample cases rather than retail replacement orders.
Lead time is confirmed after the technical definition is clear. Standard parts are typically planned at 10–25 business days, custom components at 20–45 business days, and project-based assemblies or related equipment at 45–120 business days where applicable. EXW, FOB, CIF and DAP are commonly supported; FCA, CFR, CPT, CIP and DDP can be discussed for suitable shipments. Treat these as planning ranges, not a shipment promise before order review.
A Practical Decision Sequence
Start with measurement datum, shaft fit, hub condition and controlled runout requirement. Keep the machine requirement separate from the catalogue choice: first identify what the drive must preserve, then compare only the rows or drawings that match that identity. This keeps a familiar-looking pulley from being accepted before its functional interfaces have been checked.
For an existing machine, preserve the original relationship before making changes. For a new design, record the target ratio, operating context and installation envelope so the runout review can be reviewed later without relying on memory or a photograph alone.
Build a Measurement Record
The most useful measurement set contains measurement method, datum, shaft/hub fit, observed runout and required limit if controlled. Mark which values were measured on the machine and which values came from a catalogue or released drawing. When a feature is inaccessible, photograph its relationship to a stable datum and identify it as confirmation-required rather than filling the gap with an assumed value.
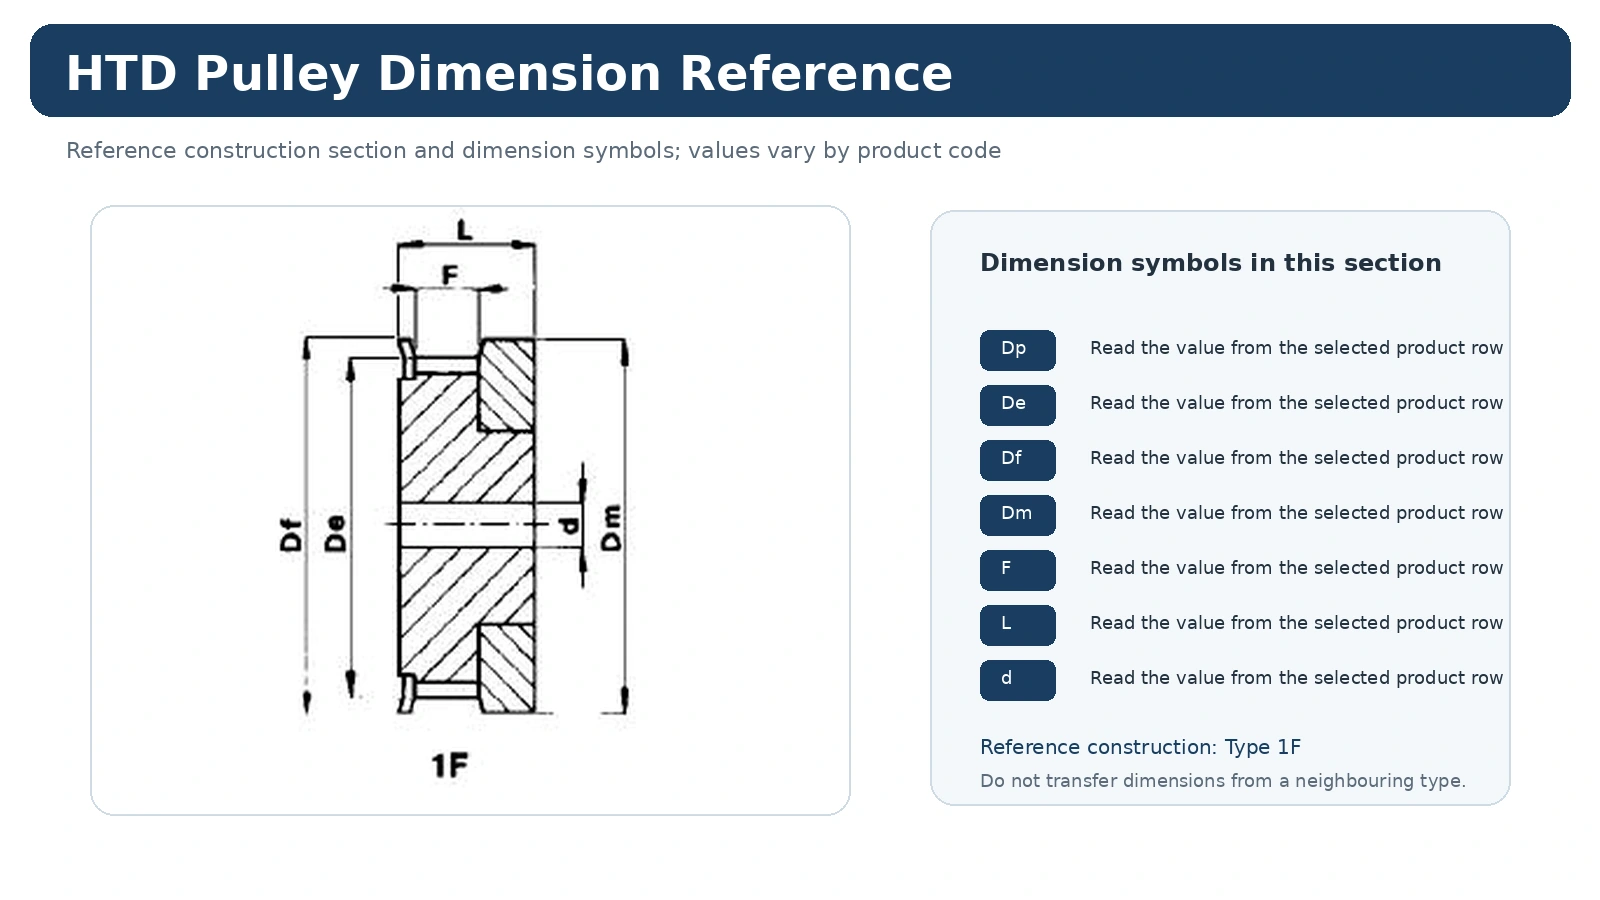
Dimension drawings should be viewed at full readable width. Never scale a screenshot and then treat the scaled dimension as a measurement; use the printed value and the correct construction type.
One Failure Mode Worth Avoiding
A common error is quoting a universal runout value without a drawing or equipment requirement. That can produce a part that appears close in the catalogue yet changes ratio, belt line, mounting or service access. Resolve the conflicting feature before requesting price so the quotation refers to one mechanically coherent configuration.
If two candidate configurations remain possible, send both the machine measurements and photographs and the preferred option. The quotation can then identify which interface still needs confirmation instead of silently converting uncertainty into a specification.
Turn the Technical Choice Into a Quote-Ready Line Item
State the HTD/profile family and complete belt information.
Provide the tooth count, working width and relevant dimension or drawing references.
Define the bore or bush, shaft data, hub projection and belt-line position where applicable.
Add quantity, destination, required documents and the drawing revision used for the request.
When one item above is genuinely unknown, label it for confirmation. A precise open question is more useful than a plausible value that was never measured.
Questions Buyers Commonly Ask
What should be confirmed first?
Confirm measurement datum, shaft fit, hub condition and controlled runout requirement. That prevents later dimensions from being compared across the wrong product family or installation route.
What information is most useful for a replacement?
Send measurement method, datum, shaft/hub fit, observed runout and required limit if controlled, plus clear photographs before the old pulley is removed. The photographs preserve axial orientation and neighboring clearances that a loose part cannot show.
When should a drawing be used?
Use a controlled drawing whenever the catalogue row does not completely define the shaft interface, hub/flange arrangement, finish, tolerance or inspection requirement that matters to the machine.
Diagnose the System Before Replacing the Pulley
Tracking, edge wear, noise or repeated belt damage can have more than one cause. Before ordering a new pulley, inspect alignment, shaft and bearing condition, mounting security, belt condition, contamination and the position of the belt relative to the flanges. A visible symptom at the pulley is not by itself proof that the pulley geometry is the root cause.
For replacement work, document the installed condition first. Photograph both pulley faces and the belt path, record the belt marking and tooth count, and note whether the symptom appears under load, on reversal or after warm-up. Those observations make it easier to separate an installation problem from a worn or incorrect component.
Turn the Finding Into a Controlled Repair
If a pulley is replaced, keep the accepted model or drawing revision with the maintenance record. Record any shaft or hub machining performed during the repair so the next replacement does not assume the original catalogue interface still exists. If runout or a dimensional characteristic is functionally critical, define the measurement reference and acceptance value on the repair drawing or purchase requirement.
After installation, verify belt line and the drive condition before the machine returns to normal service. The goal is not simply to fit a new component; it is to restore a traceable and serviceable drive configuration.
Specify Runout Only From a Defined Datum and Functional Need
Runout and concentricity are meaningful only when the measured surface, datum and inspection method are defined. A blanket “high precision” requirement is not actionable. If radial or axial runout matters to the machine, identify the shaft/bore datum and the surface to be checked on the drawing, then state the acceptance value required by the project.
For replacement investigation, first determine whether apparent pulley wobble comes from the pulley, the shaft, the mounting interface or accumulated debris. Inspect the bore or bush and shaft condition, then check the pulley from a repeatable setup. A damaged shaft or loose bush can produce motion that would be misdiagnosed if only the outer rim is observed while running.
Catalogue dimensions remain the component reference, while project-specific inspection limits belong to the order drawing. Keeping these roles separate avoids publishing a universal tolerance that may not apply across materials, diameters or construction types.
Define Runout by Datum, Location and Measurement Method
Runout and concentricity are meaningful only when the measurement reference is clear. A buyer who needs a controlled value should identify the datum—such as a finished bore or another drawing-defined surface—the feature being checked and the measurement method. A generic “high precision” note is not an inspectable requirement.
Field measurements on a worn assembly can be influenced by shaft condition, bearing play, debris or mounting error. Before attributing measured runout to the pulley itself, inspect those factors and record the test setup. If a specific acceptance value is required, it should come from the machine design, component drawing or agreed order requirement.
State the surface or axis from which the measurement is referenced.
Identify the diameter, face or belt-running surface being checked.
Describe indicator position or inspection method when the result is order-critical.
Put the accepted value on the drawing or RFQ instead of using a universal website claim.
For replacement troubleshooting, compare the old and new components on the same shaft or controlled fixture where practical. This makes the result more useful than two measurements taken from different setups.