HTD 8M Timing Pulley Selection Guide should be approached as a drive-system decision. The useful starting point is the mating belt and machine interface, followed by tooth count, working width, shaft mounting and duty conditions. This guide explains the checks that help an engineer or buyer turn HTD 8M timing pulley selection into an RFQ that can be verified against a catalogue row or drawing.
Identify the Drive Before Comparing Dimensions
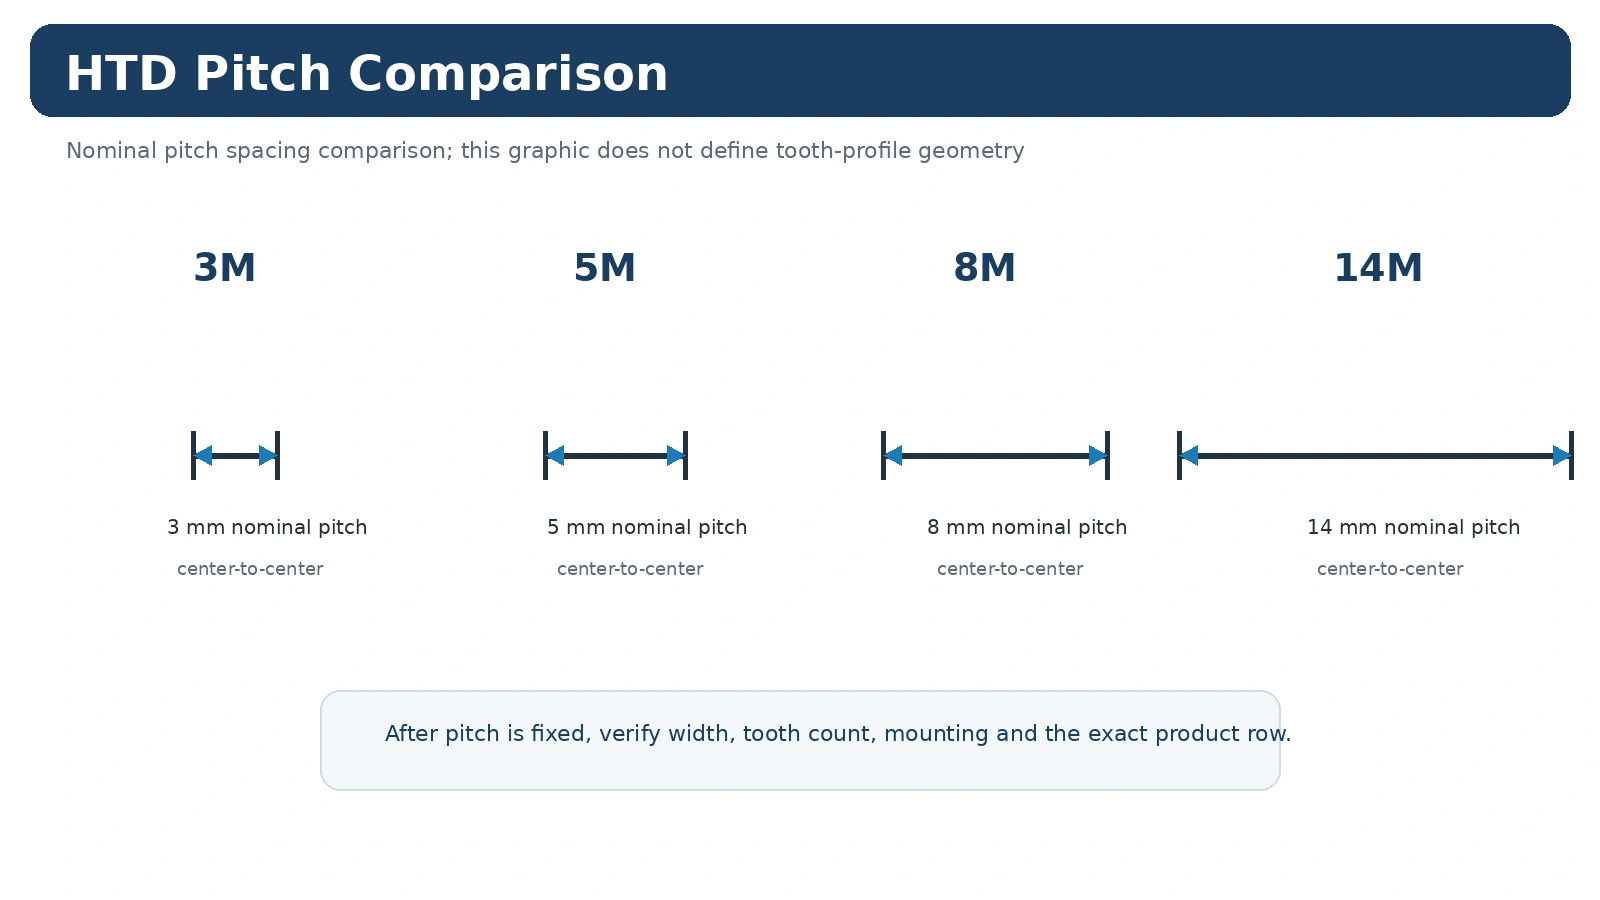
For HTD 8M timing pulley selection, identify the complete belt marking before comparing pulley diameters. HTD is a curvilinear synchronous system and the nominal pitch must stay associated with its profile family. Record the driver and driven tooth counts when an existing ratio must be preserved. For a new drive, document the target speed ratio, driver speed and expected load before choosing tooth counts. This prevents a component-level decision from overriding the machine requirement.
For a replacement project, compare the measured value with the installed belt and machine arrangement before deciding that a catalogue row is equivalent. For a new project, document the design basis so later maintenance teams can understand why the pitch, tooth count and mounting style were selected.
Dimensions That Control the Installation
A pulley can match pitch and tooth count yet still fail to fit the machine because the bore, hub, flange or axial position differs. Measure the shaft interface, belt-face width, hub projection on both sides and the belt line relative to a stable machine datum. Where a taper bush is used, record both the pulley series and bush code. Where a finished bore is required, include fit, keyway and any retaining method on the drawing.
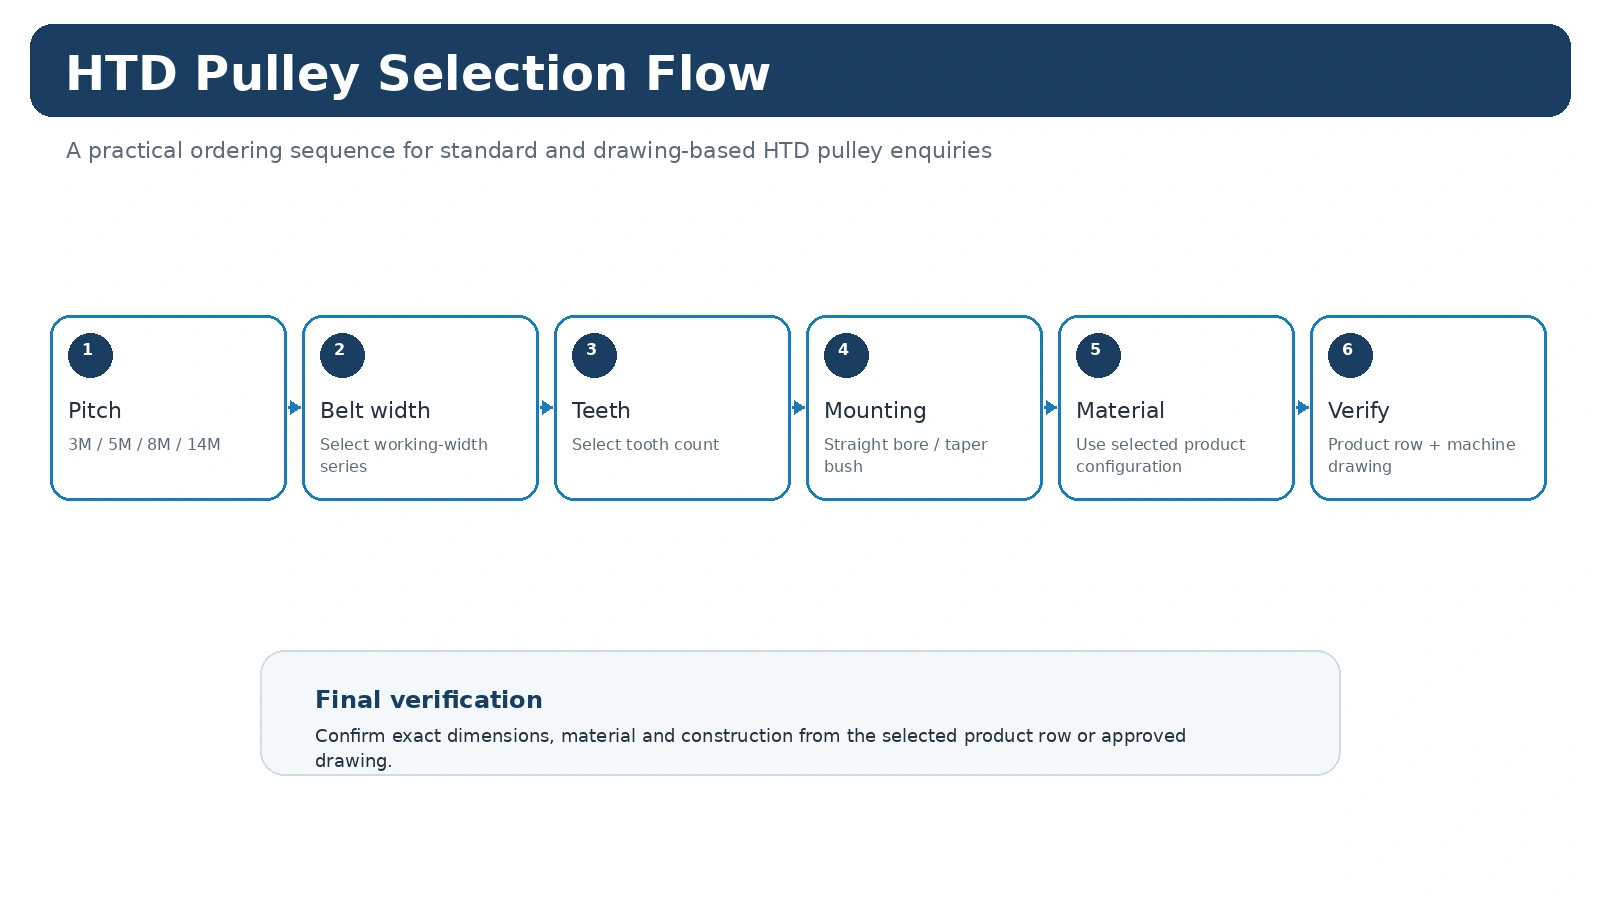
For a replacement project, compare the measured value with the installed belt and machine arrangement before deciding that a catalogue row is equivalent. For a new project, document the design basis so later maintenance teams can understand why the pitch, tooth count and mounting style were selected.
Operating Conditions That Belong in the Selection
The same nominal HTD 8M timing pulley selection component can see very different service depending on the machine. Starts per hour, reversing, shock loading, continuous operating time, temperature, contamination, cleaning and access for tensioning all influence the drive. A compact automation axis emphasizes repeatable motion and controlled alignment, while a conveyor or process machine may emphasize continuous duty and service access. Supply these conditions instead of asking the pulley to be selected from size alone.
For a replacement project, compare the measured value with the installed belt and machine arrangement before deciding that a catalogue row is equivalent. For a new project, document the design basis so later maintenance teams can understand why the pitch, tooth count and mounting style were selected.
Inspection Points Before Installation
Inspection should focus on dimensions that affect the drive: the shaft interface, axial location, tooth condition, face width and any drawing-controlled runout or datum relationship. A generic quality statement does not define acceptance. If a dimensional report, material document or order-specific record is required, identify it before production. During maintenance, watch for flange damage, edge wear, debris and signs that the pulley has moved on the shaft.
For a replacement project, compare the measured value with the installed belt and machine arrangement before deciding that a catalogue row is equivalent. For a new project, document the design basis so later maintenance teams can understand why the pitch, tooth count and mounting style were selected.
Open Questions to Close Before Ordering
What exact HTD profile and width is installed or specified?
What ratio or existing tooth count must be preserved?
What bore, fit, keyway or taper-bush arrangement is required?
How much hub projection and flange clearance is available?
What are the speed, load, starts, reversing and operating hours?
Which drawing, material or inspection records must accompany supply?
What to Send With the RFQ
Send profile, tooth count, belt width, shaft interface, hub/flange details, quantity, destination and a drawing or replacement measurement sketch. Add speed, ratio, load, center distance and environment for a new drive. Review the HTD product families, use the selection guide, or compare the relevant application notes.
8M Selection Priorities
The 8M range is organised as 8M-20, 8M-30, 8M-50 and 8M-85. Larger diameters and hubs make shaft interface, axial space and handling increasingly important as tooth count grows.
Keep measured values, catalogue references and project requirements clearly separated. If a required point is not stated in the relevant catalogue table or approved drawing, include it as an RFQ question or drawing requirement instead of filling the gap with a plausible but unverified value.
Separate Straight-Bore and Taper-Bush Choices
Both mounting routes exist in supported 8M families, but they are not the same product. Keep the selected construction and any bush designation with the tooth-count row.
The purchasing record should keep a clear link between the machine requirement and the selected pulley. That means the complete belt or profile identity, tooth count, working width and shaft-interface information remain together with the product code. Any special material, finish, controlled tolerance, marking or report requirement should be stated separately so it cannot be mistaken for a universal feature of the whole family.
Procurement and Documentation
Once the selection is clear, keep the accepted product identity, quantity, destination and drawing revision on the same purchase line. Standard catalogue parts are normally planned around production-quantity minimums, while larger or higher-value items can be reviewed against the practical order value. Qualified new-client samples of 1–5 pieces may be reviewed at sample pricing when the configuration and manufacturing route are suitable.
Mixed-model orders can be consolidated toward a practical order value of about USD 1,500. Special materials and special processes follow the minimum quantity required by that process. Very small one- or two-piece requests are handled only as qualified engineering validation or paid-sample cases rather than retail replacement orders.
Lead time is confirmed after the technical definition is clear. Standard parts are typically planned at 10–25 business days, custom components at 20–45 business days, and project-based assemblies or related equipment at 45–120 business days where applicable. EXW, FOB, CIF and DAP are commonly supported; FCA, CFR, CPT, CIP and DDP can be discussed for suitable shipments. Treat these as planning ranges, not a shipment promise before order review.
A Practical Decision Sequence
Start with 8 mm HTD family, width code, tooth count and shaft interface. Keep the machine requirement separate from the catalogue choice: first identify what the drive must preserve, then compare only the rows or drawings that match that identity. This keeps a familiar-looking pulley from being accepted before its functional interfaces have been checked.
For an existing machine, preserve the original relationship before making changes. For a new design, record the target ratio, operating context and installation envelope so the 8M selection can be reviewed later without relying on memory or a photograph alone.
Build a Measurement Record
The most useful measurement set contains 8M belt marking, tooth count, width series, construction type and bore/bush. Mark which values were measured on the machine and which values came from a catalogue or released drawing. When a feature is inaccessible, photograph its relationship to a stable datum and identify it as confirmation-required rather than filling the gap with an assumed value.
Dimension drawings should be viewed at full readable width. Never scale a screenshot and then treat the scaled dimension as a measurement; use the printed value and the correct construction type.
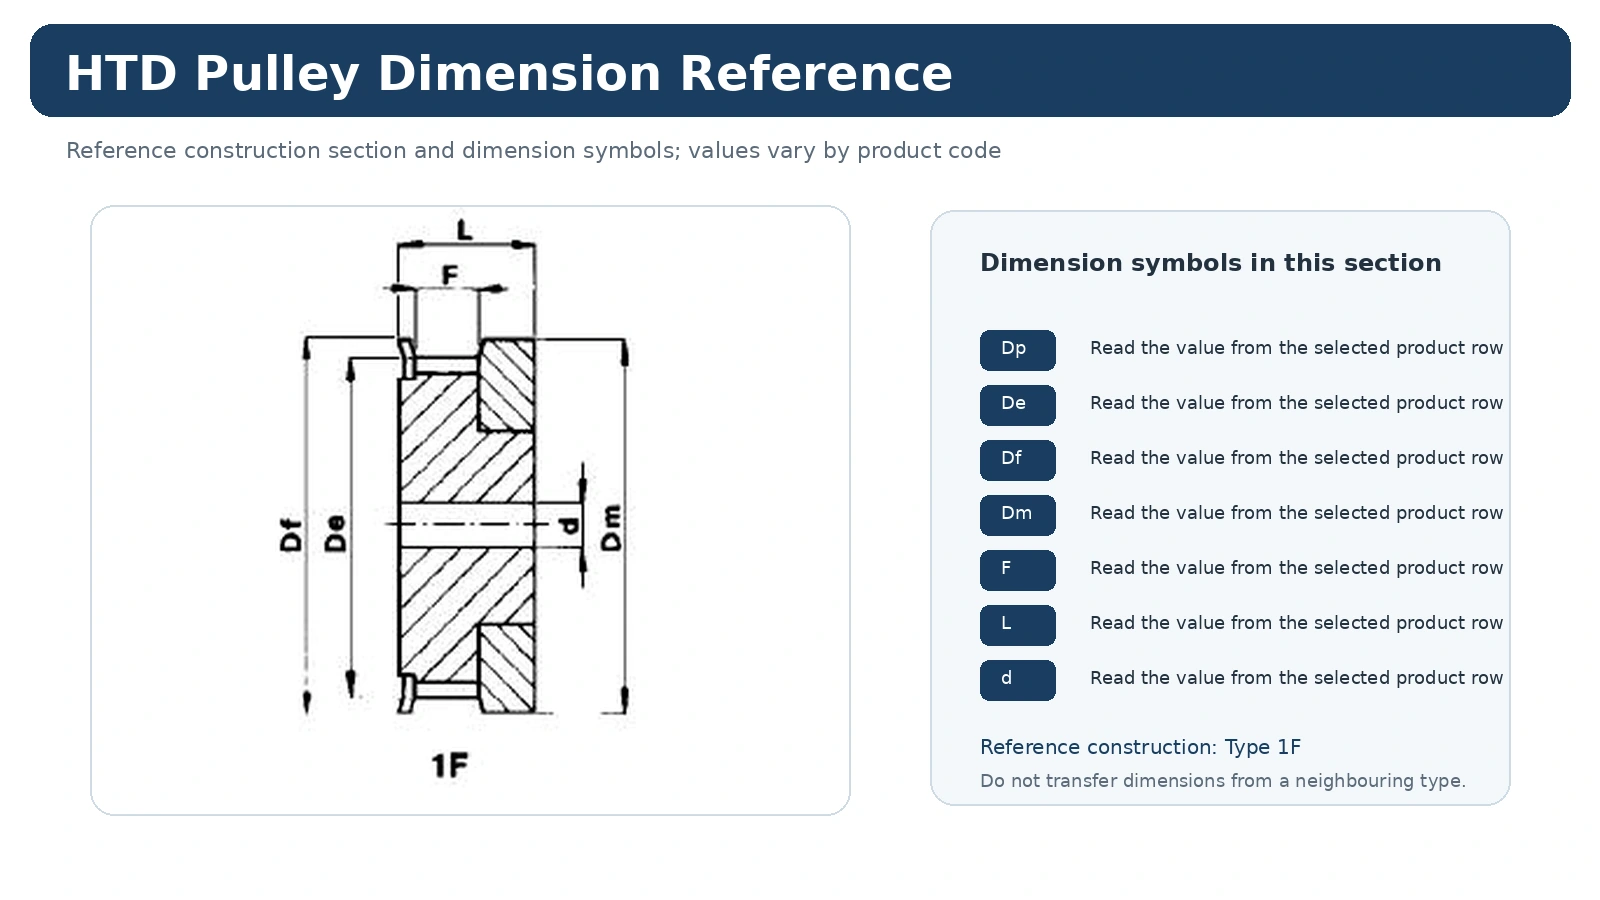
One Failure Mode Worth Avoiding
A common error is choosing from pitch diameter while ignoring construction type. That can produce a part that appears close in the catalogue yet changes ratio, belt line, mounting or service access. Resolve the conflicting feature before requesting price so the quotation refers to one mechanically coherent configuration.
If two candidate configurations remain possible, send both the machine measurements and photographs and the preferred option. The quotation can then identify which interface still needs confirmation instead of silently converting uncertainty into a specification.
Turn the Technical Choice Into a Quote-Ready Line Item
State the HTD/profile family and complete belt information.
Provide the tooth count, working width and relevant dimension or drawing references.
Define the bore or bush, shaft data, hub projection and belt-line position where applicable.
Add quantity, destination, required documents and the drawing revision used for the request.
When one item above is genuinely unknown, label it for confirmation. A precise open question is more useful than a plausible value that was never measured.
Questions Buyers Commonly Ask
What should be confirmed first?
Confirm 8 mm HTD family, width code, tooth count and shaft interface. That prevents later dimensions from being compared across the wrong product family or installation route.
What information is most useful for a replacement?
Send 8M belt marking, tooth count, width series, construction type and bore/bush, plus clear photographs before the old pulley is removed. The photographs preserve axial orientation and neighboring clearances that a loose part cannot show.
When should a drawing be used?
Use a controlled drawing whenever the catalogue row does not completely define the shaft interface, hub/flange arrangement, finish, tolerance or inspection requirement that matters to the machine.
Pitch Family Is Only the First Branch of the Selection
8M selection still requires working width, tooth count and mounting geometry. Tooth count changes pitch diameter and can also coincide with changes in body type, hub and material across a catalogue family. The correct comparison therefore stays row-specific after the pitch has been chosen. For a new drive, ratio and center distance must be reviewed together with available diameter and guard clearance.
For a replacement, begin with the mating belt and the installed part. If the belt identity is uncertain, avoid choosing a new family only because the measured pitch appears close. Obtain enough measurements and identification detail to identify the tooth system before comparing product rows.
When to Escalate From a Catalogue Row to a Drawing
Use a drawing-controlled order when the shaft connection, hub position, flange arrangement, material, finish or inspection requirement differs from the normal catalogue configuration. Keep standard HTD tooth geometry explicit on the drawing so the custom machining request does not accidentally obscure the mating-belt requirement.
On mixed-model RFQs, keep every width and tooth count on its own line. A general note such as “same as above” can become unsafe once one model uses a different construction type or bush.
Compare the 8M Row Against the Installed Envelope
An 8M replacement should be compared in a simple sequence: first the belt-side identity, then the radial envelope, then the axial envelope. Confirm the 8M belt marking and working width, count the pulley teeth, and compare the corresponding catalogue row. Next check the diameter-related clearances to guards and adjacent components. Finally compare hub projection, overall width and shaft interface from both sides. This sequence is useful because a part can agree with the first two checks yet still move the belt line when the hub arrangement differs.
If the machine uses a taper-bush version, include the bush marking, shaft diameter and installation direction in the same record. Do not treat the bush as a separate purchasing accessory once the pulley row has been chosen; the supported combination is part of the mounting geometry. For straight-bore work, mark any finished bore or keyway requirement on the drawing if it is not already defined by the standard row.
When evaluating a new 8M drive, add the intended speed relationship, center distance, duty pattern and available service space. These inputs do not create a universal rating; they tell the supplier which machine-side constraints must be considered alongside the published component geometry.
Keep 8M Width Series and Tooth Count on the Same Purchase Line
For mixed 8M enquiries, write the width series and tooth count together for every model instead of using a shared note such as “same as above.” The 8M-20, 8M-30, 8M-50 and 8M-85 families do not describe one interchangeable body. Construction type, material and mounting details can change with the individual row, so each order line should preserve the complete identification used during comparison.
If a replacement is being sourced from photographs, use those photographs to establish orientation and surrounding clearance, not to infer hidden dimensions. Confirm the belt marking and take the shaft-side measurements before the old component is discarded. Where a standard row still leaves a machine-specific fit or tolerance undefined, attach the drawing requirement to that exact line.
Review the Larger 8M Envelope Together With Hub and Shaft Requirements
The 8M range includes 8M-20, 8M-30, 8M-50 and 8M-85 width-series pages in both straight-bore and selected taper-bush configurations. As tooth count increases, the pulley envelope and construction details can change substantially, so the model table should be read row by row rather than treated as one generic 8M pulley.
For replacements, record hub projection, flange position and shaft interface in addition to tooth count. Larger pulleys often sit close to guards, bearing housings or adjacent drive elements, and a seemingly minor axial change can prevent installation. For new designs, confirm service access and removal space before the surrounding machine layout is frozen.
Narrower 8M width families; compare exact construction type by tooth count.
Wider 8M families with larger axial envelopes.
Keep mounting family and shaft data with the selected product code.
Put any controlled runout, finish or document requirement on the RFQ or drawing.
Use the 8M page as a catalogue map, not as a universal performance claim. Drive sizing remains tied to the belt system and application conditions; the pulley table controls the geometry and ordering identity.