HTD-kugghjul för verktygsmaskiner should be approached as a drive-system decision. The useful starting point is the mating belt and machine interface, followed by tooth count, working width, shaft mounting and duty conditions. This guide explains the checks that help an engineer or buyer turn timing pulley machine tools into an RFQ that can be verified against a catalogue row or drawing.
Identifiera drivenheten innan du jämför dimensioner
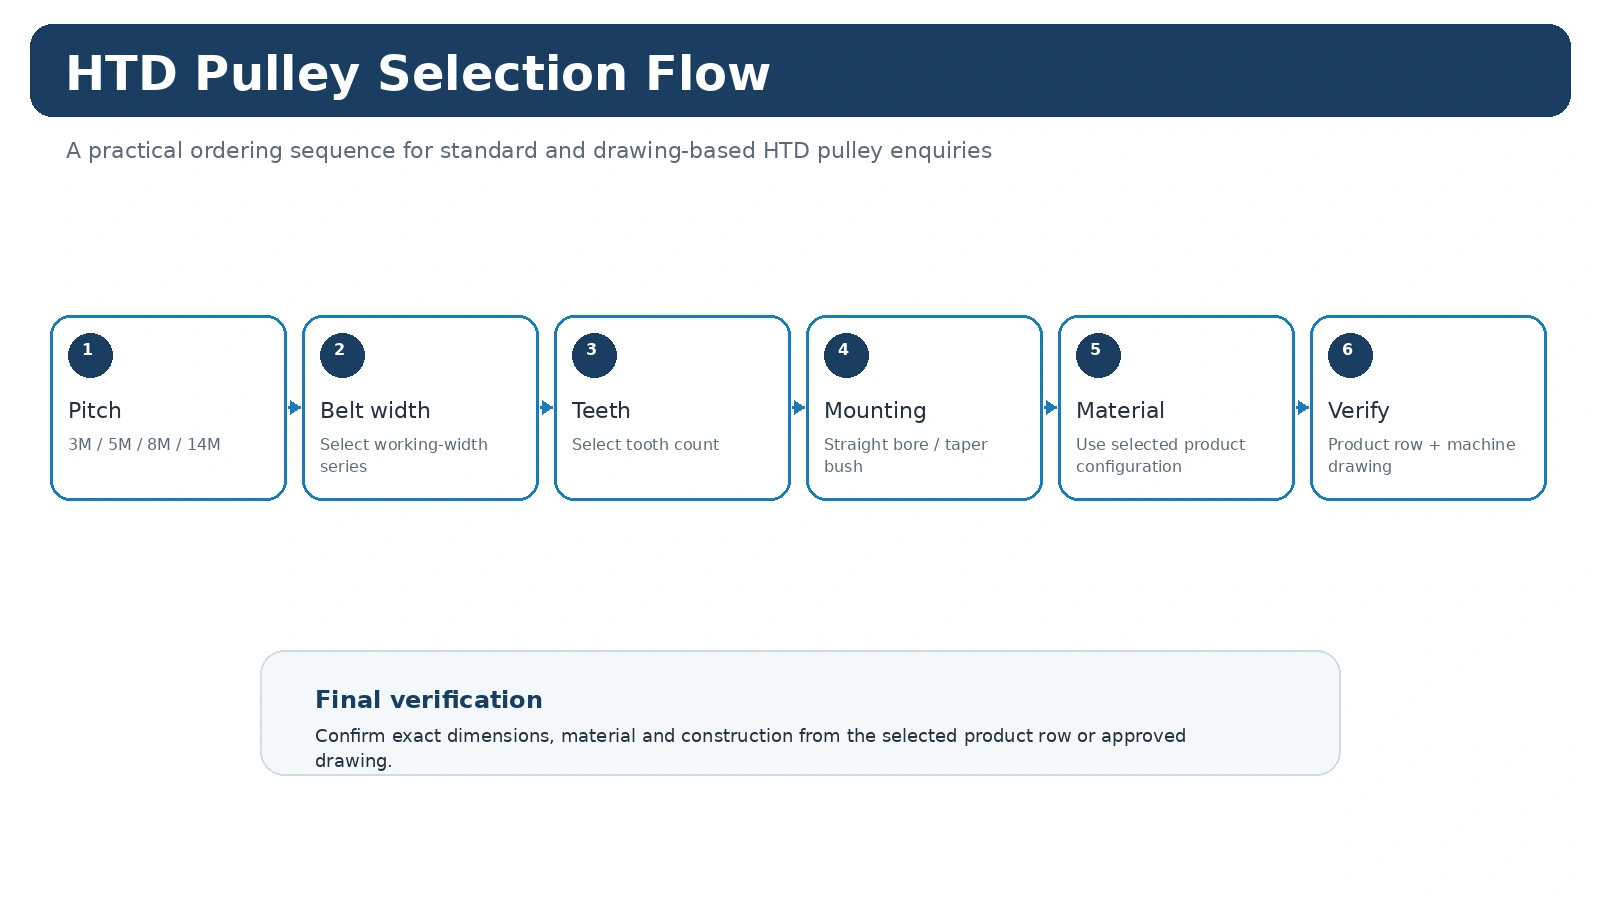
For timing pulley machine tools, identify the complete belt marking before comparing pulley diameters. HTD is a curvilinear synchronous system and the nominal pitch must stay associated with its profile family. Record the driver and driven tooth counts when an existing ratio must be preserved. For a new drive, document the target speed ratio, driver speed and expected load before choosing tooth counts. This prevents a component-level decision from overriding the machine requirement.
För ett ersättningsprojekt, jämför det uppmätta värdet med det installerade bandet och maskinarrangemanget innan du bestämmer att en katalograd är likvärdig. För ett nytt projekt, dokumentera konstruktionsunderlaget så att senare underhållsteam kan förstå varför stigning, tandantal och monteringsstil valdes.
Mått som styr installationen
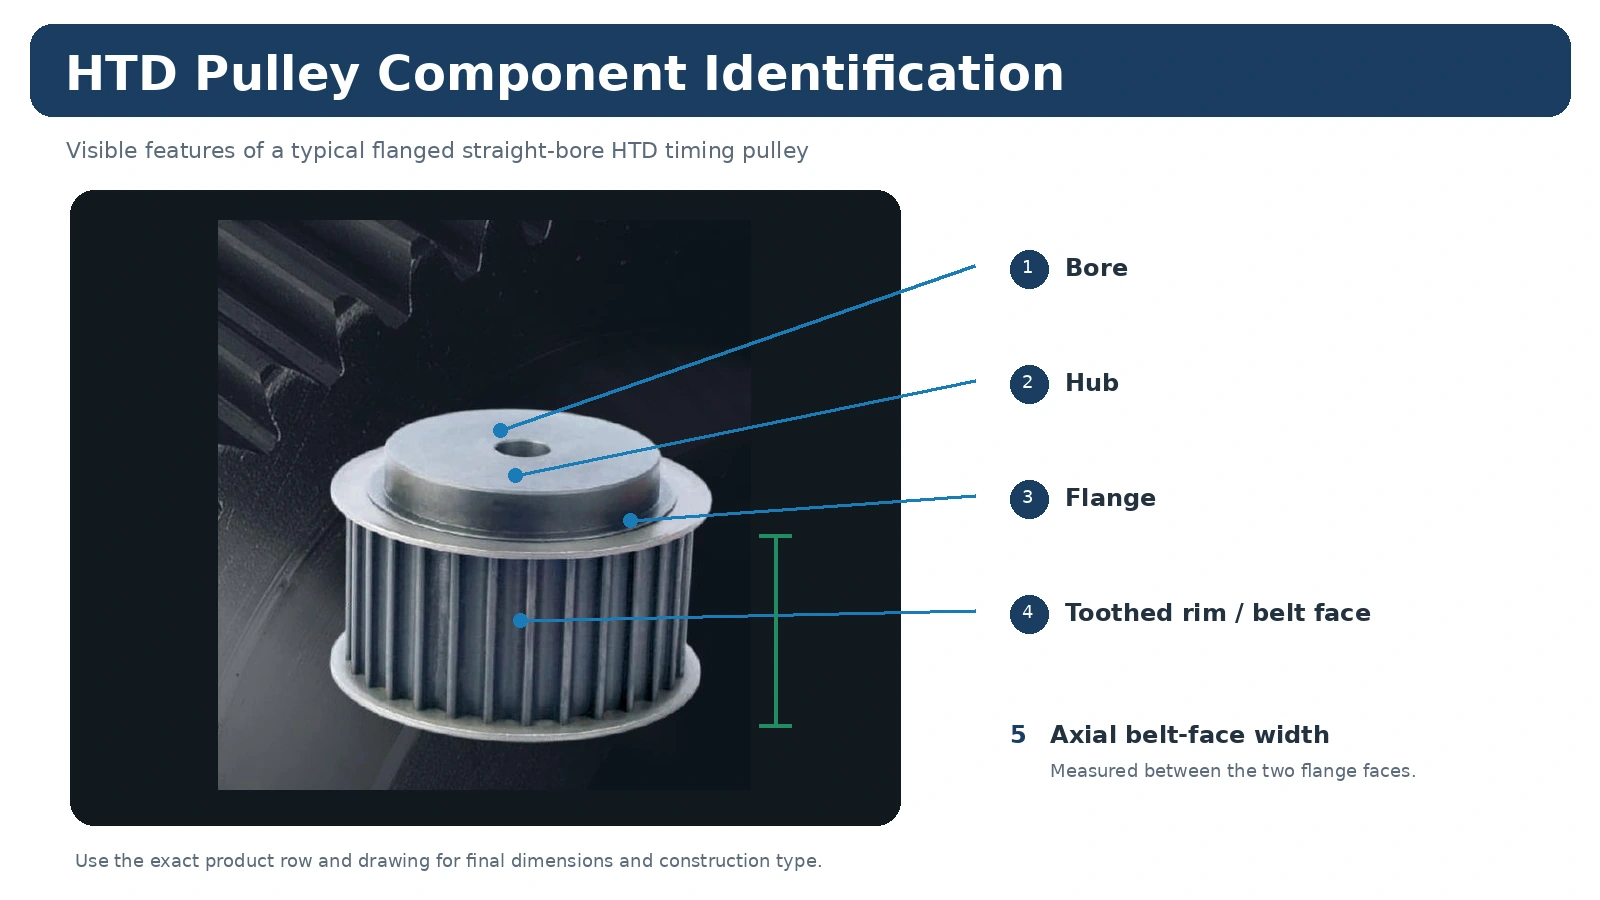
En remskiva kan matcha stigning och kuggantal men ändå inte passa maskinen eftersom borrningen, navet, flänsen eller den axiella positionen skiljer sig åt. Mät axelgränssnittet, remytans bredd, navprojektionen på båda sidor och remlinjen i förhållande till ett stabilt maskinutgångspunkt. Om en konisk bussning används, registrera både remskivans serie och bussningskod. Om ett färdigt borrhål krävs, inkludera passform, kilspår och eventuell fasthållningsmetod på ritningen.
För ett ersättningsprojekt, jämför det uppmätta värdet med det installerade bandet och maskinarrangemanget innan du bestämmer att en katalograd är likvärdig. För ett nytt projekt, dokumentera konstruktionsunderlaget så att senare underhållsteam kan förstå varför stigning, tandantal och monteringsstil valdes.
Driftsförhållanden som hör hemma i urvalet
The same nominal timing pulley machine tools component can see very different service depending on the machine. Starts per hour, reversing, shock loading, continuous operating time, temperature, contamination, cleaning and access for tensioning all influence the drive. A compact automation axis emphasizes repeatable motion and controlled alignment, while a conveyor or process machine may emphasize continuous duty and service access. Supply these conditions instead of asking the pulley to be selected from size alone.

För ett ersättningsprojekt, jämför det uppmätta värdet med det installerade bandet och maskinarrangemanget innan du bestämmer att en katalograd är likvärdig. För ett nytt projekt, dokumentera konstruktionsunderlaget så att senare underhållsteam kan förstå varför stigning, tandantal och monteringsstil valdes.
Inspektionspunkter före installation
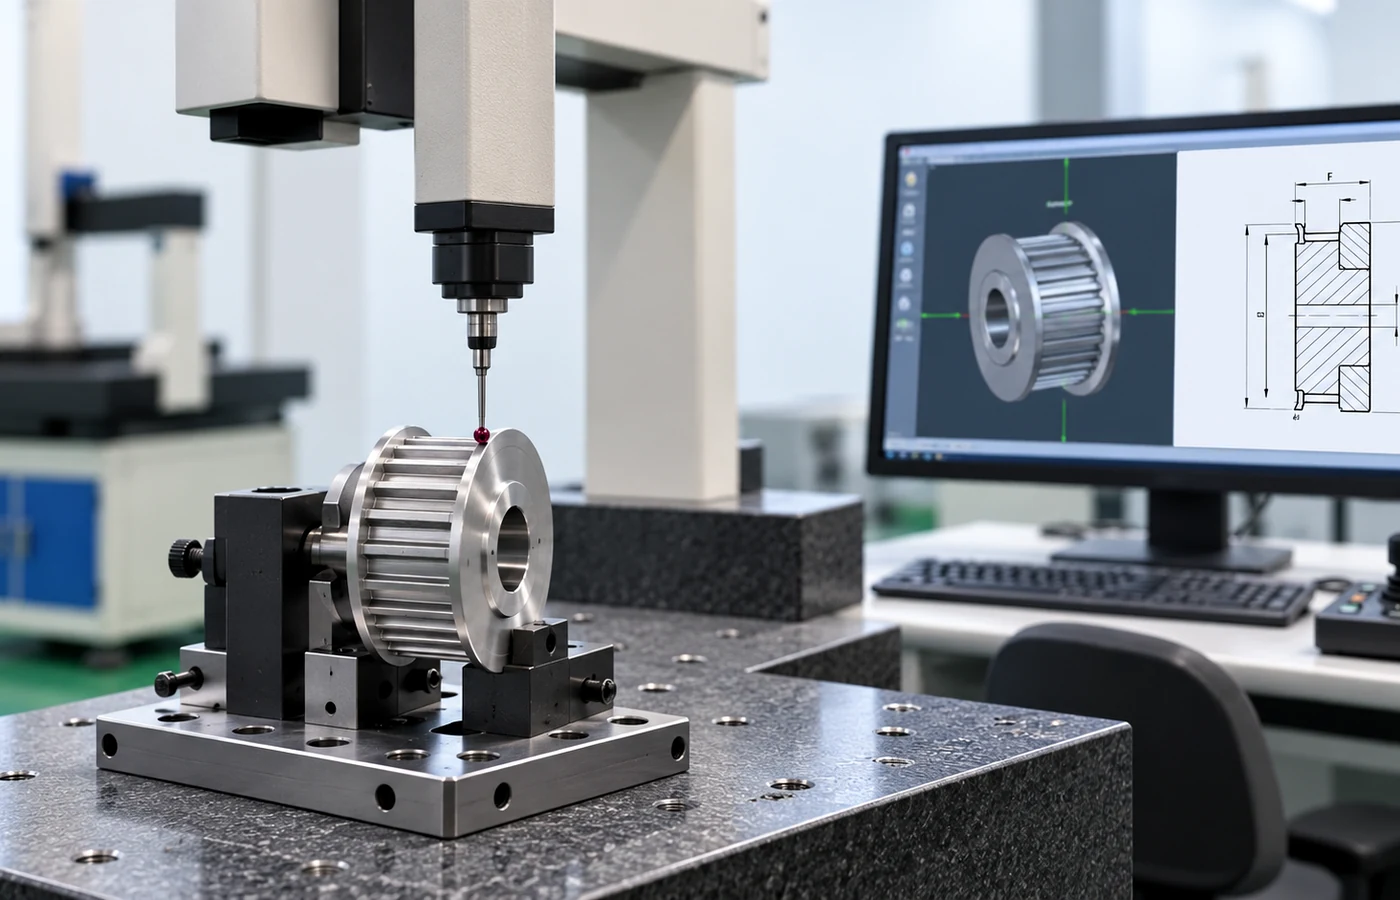
Inspektionen bör fokusera på dimensioner som påverkar drivningen: axelgränssnittet, axiellt läge, tandskick, planbredd och eventuella ritningsstyrda rundgångs- eller utgångsförhållanden. En generell kvalitetsdeklaration definierar inte godkännande. Om en dimensionsrapport, ett materialdokument eller en orderspecifik registrering krävs, identifiera den före produktion. Under underhåll, var uppmärksam på flänsskador, kantslitage, skräp och tecken på att remskivan har rört sig på axeln.
För ett ersättningsprojekt, jämför det uppmätta värdet med det installerade bandet och maskinarrangemanget innan du bestämmer att en katalograd är likvärdig. För ett nytt projekt, dokumentera konstruktionsunderlaget så att senare underhållsteam kan förstå varför stigning, tandantal och monteringsstil valdes.
Öppna frågor att stänga innan beställning
Vilken exakt HTD-profil och bredd är installerad eller specificerad?
Vilket förhållande eller befintligt tandantal måste bevaras?
Vilket arrangemang för hål, passning, kilspår eller konisk bussning krävs?
Hur mycket navutskjutande och flänsspel finns tillgängligt?
Vad är hastigheten, belastningen, starterna, reverseringen och driftstimmarna?
Vilka ritningar, material eller inspektionsprotokoll måste medfölja leveransen?
Vad som ska skickas med offerten
Skicka profil, kuggantal, rembredd, axelgränssnitt, nav-/flänsdetaljer, kvantitet, destination och en ritning eller måttskiss för ersättning. Lägg till hastighet, utväxling, belastning, centrumavstånd och miljö för en ny drivning. Granska HTD-produktfamiljer, använd urvalsguide, eller jämför relevanta applikationsanteckningar.
Machine-Tool Drives Need Controlled Geometry
Auxiliary axes, feeders and machine-tool mechanisms can be sensitive to belt line, pulley runout and shaft fit. Put any controlled tolerance on the drawing rather than using a universal value copied from another machine.
Capture operating hours, starts and stops, reversal if present, nearby guards and the condition of the shaft support. These details provide the application context for the pulley without turning the page into an unsupported power or life-rating claim.
Keep Lubrication and Chip Exposure in the RFQ
Describe coolant, chip, oil or enclosure conditions around the drive. The application context can influence material, guarding and maintenance planning even when the catalogue pulley geometry itself is unchanged.
Inköpsregistret bör ha en tydlig koppling mellan maskinkravet och den valda remskivan. Det innebär att den fullständiga rem- eller profilidentiteten, kuggantalet, arbetsbredden och informationen om axelgränssnittet bibehålls tillsammans med produktkoden. Eventuella speciella material, ytbehandlingar, kontrollerade toleranser, märknings- eller rapportkrav bör anges separat så att de inte kan misstas för en universell egenskap hos hela familjen.
Upphandling och dokumentation
När valet är klart, behåll den accepterade produktidentiteten, kvantiteten, destinationen och ritningsrevisionen på samma inköpsrad. Standardartiklar i katalogen planeras normalt kring produktionskvantitet, medan större eller mer värdefulla artiklar kan granskas mot det praktiska ordervärdet. Kvalificerade prover från nya kunder på 1–5 stycken kan granskas till provpris när konfigurationen och tillverkningsvägen är lämpliga.
Blandade modellbeställningar kan konsolideras till ett praktiskt ordervärde på cirka 1 500 USD. Specialmaterial och specialprocesser följer den minsta kvantitet som krävs av den processen. Mycket små förfrågningar om en eller två stycken hanteras endast som kvalificerad teknisk validering eller betalda prover snarare än ersättningsbeställningar från detaljhandeln.
Ledtiden bekräftas efter att den tekniska definitionen är tydlig. Standarddelar planeras vanligtvis till 10–25 arbetsdagar, specialkomponenter till 20–45 arbetsdagar och projektbaserade monteringar eller relaterad utrustning till 45–120 arbetsdagar där så är tillämpligt. EXW, FOB, CIF och DAP stöds vanligtvis; FCA, CFR, CPT, CIP och DDP kan diskuteras för lämpliga leveranser. Behandla dessa som planeringsintervall, inte ett leveranslöfte före ordergranskning.
En praktisk beslutssekvens
Start with positioning duty, spindle/axis speed relationship and installation stiffness. Keep the machine requirement separate from the catalogue choice: first identify what the drive must preserve, then compare only the rows or drawings that match that identity. This keeps a familiar-looking pulley from being accepted before its functional interfaces have been checked.
For an existing machine, preserve the original relationship before making changes. For a new design, record the target ratio, operating context and installation envelope so the machine-tool drive definition can be reviewed later without relying on memory or a photograph alone.
Skapa en mätjournal
The most useful measurement set contains speed ratio, duty, pitch family, width, shaft fit and runout requirement if controlled. Mark which values were measured on the machine and which values came from a catalogue or released drawing. When a feature is inaccessible, photograph its relationship to a stable datum and identify it as confirmation-required rather than filling the gap with an assumed value.
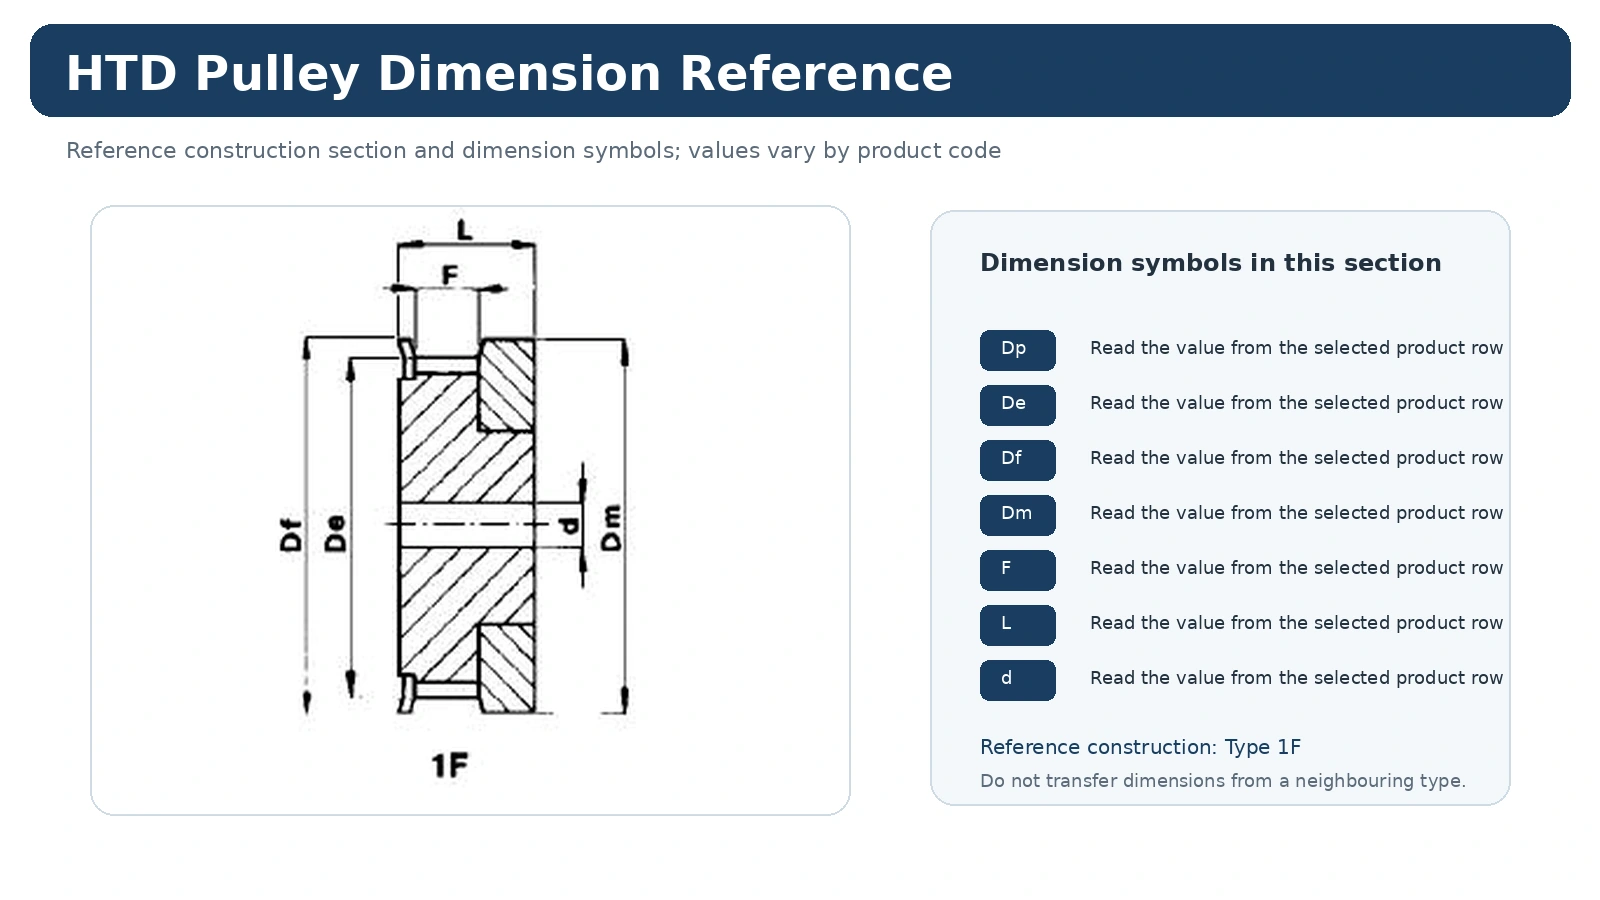
Måttritningar bör visas i full läsbar bredd. Skala aldrig en skärmdump och behandla sedan den skalade måtten som ett mått; använd det utskrivna värdet och rätt konstruktionstyp.
Ett felläge värt att undvika
A common error is treating a precision axis as a generic conveyor drive. That can produce a part that appears close in the catalogue yet changes ratio, belt line, mounting or service access. Resolve the conflicting feature before requesting price so the quotation refers to one mechanically coherent configuration.
Om två möjliga konfigurationer fortfarande är möjliga, skicka både maskinmått och fotografier samt det föredragna alternativet. Offerten kan då identifiera vilket gränssnitt som fortfarande behöver bekräftelse istället för att i tysthet omvandla osäkerhet till en specifikation.
Förvandla det tekniska valet till en offertklar radartikel
Ange HTD/profilfamilj och komplettera reminformationen.
Ange antal tänder, arbetsbredd och relevanta mått eller ritningsreferenser.
Definiera borrning eller bussning, axeldata, navutskjutning och remlinjens position där så är tillämpligt.
Lägg till kvantitet, destination, nödvändiga dokument och den ritningsrevision som används för begäran.
När en punkt ovan är genuint okänd, markera den för bekräftelse. En precis öppen fråga är mer användbar än ett rimligt värde som aldrig mättes.
Frågor som köpare ofta ställer
Vad bör bekräftas först?
Confirm positioning duty, spindle/axis speed relationship and installation stiffness. That prevents later dimensions from being compared across the wrong product family or installation route.
Vilken information är mest användbar för en ersättning?
Send speed ratio, duty, pitch family, width, shaft fit and runout requirement if controlled, plus clear photographs before the old pulley is removed. The photographs preserve axial orientation and neighboring clearances that a loose part cannot show.
När ska en ritning användas?
Använd en kontrollerad ritning närhelst katalograden inte fullständigt definierar axelgränssnittet, nav-/flänsarrangemanget, ytbehandlingen, toleransen eller inspektionskravet som är relevant för maskinen.
Machine Conditions to Record for Machine Tools
Do not select a pulley from the industry name alone. Record the operating pattern of the actual machine: driver and driven speeds or ratio, torque or power where available, center distance, hours per day, start/stop frequency, reversal, contamination and the available guard/shaft envelope. These details explain the duty without turning a general article into an unsupported product rating.
For maintenance replacement, add the installed belt marking, tooth count, working face, hub projection and shaft interface. If there has been edge wear or tracking trouble, capture the belt line and bearing/shaft condition before altering pulley geometry.
Installation Planning for Machine Tools
Confirm that the selected pulley can be fitted and removed with the available service access. A hub that is technically compatible can still cause downtime if adjacent bearings or guards block installation. Maintain the intended belt plane and review flange clearance so the belt is guided without using persistent flange contact as a substitute for alignment.
Where washdown, dust, fibers, chips or process residue are present, include the environment in the RFQ. Material and maintenance decisions should be reviewed against the actual configuration and environment rather than copied from another application.
Machine-Tool Drives Require the Mechanical Interface to Stay Tied to the Motion Function
Machine tools can use synchronous drives in auxiliary axes, positioning systems, conveyors and internal mechanisms. The machine category alone does not define the pulley. Start with the actual axis: identify the belt family, ratio, shaft arrangement, available diameter and the consequence of lost position or tracking error in that function.
For replacement work, preserve the relationship between pulley, shaft shoulder, spacer and guard. A visually similar pulley with a different hub projection can shift the belt plane enough to create edge loading. If runout or concentricity is a controlled characteristic, put the required inspection point and tolerance on the drawing instead of relying on a generic website statement.
For a new design, provide duty, speed relationship, center distance and environmental information with the RFQ. Those inputs allow the catalogue geometry to be assessed in the context of the actual machine rather than turned into a universal machine-tool rating.
Preserve Datum and Axial Position on Replacement Work
Machine-tool assemblies often have tight axial packaging around bearings, couplings, encoders or guards. A replacement record should therefore include a dimension from a stable shaft shoulder or housing datum to the pulley working face, not just overall pulley width. This makes it possible to detect a hub-orientation difference that a front photograph may miss.
If the old part is being reverse-measured, mark surfaces that are worn or damaged before taking final dimensions. Do not use a burred bore, fretted keyway or polished flange as the nominal geometry. Where the correct original dimension cannot be recovered from the catalogue, use a controlled drawing and identify the fit or runout requirement from the machine design.
Separate Machine Accuracy Requirements From Catalogue Geometry
Machine-tool timing drives may serve auxiliary axes, spindle-related mechanisms, tool handling or other coordinated motion. The pulley catalogue defines tooth family and physical geometry, but any machine-specific runout, fit, balance or positioning requirement must come from the equipment design or approved component drawing.
Do not add a generic “precision” tolerance to every pulley simply because the machine is a machine tool. First identify which characteristic actually affects the axis—shaft fit, axial belt line, runout at a defined datum, or another controlled dimension—then state that characteristic and how it will be inspected. This produces a requirement that can be manufactured and verified.
Identify the axis and what the timing drive does in the machine.
Define the shaft or drawing datum used for critical measurements.
Check hub projection, flange clearance and guard space.
Specify only the dimensions or records that the machine genuinely controls.
For replacement work, compare the new pulley to both the catalogue row and the installed machine. Previous repairs may have changed the shaft or hub from the original design, so the current interface should be measured rather than assumed.