قرقرههای زمانبندی HTD برای اتوماسیون صنعتی should be approached as a drive-system decision. The useful starting point is the mating belt and machine interface, followed by tooth count, working width, shaft mounting and duty conditions. This guide explains the checks that help an engineer or buyer turn timing pulley industrial automation into an RFQ that can be verified against a catalogue row or drawing.
قبل از مقایسه ابعاد، درایو را شناسایی کنید
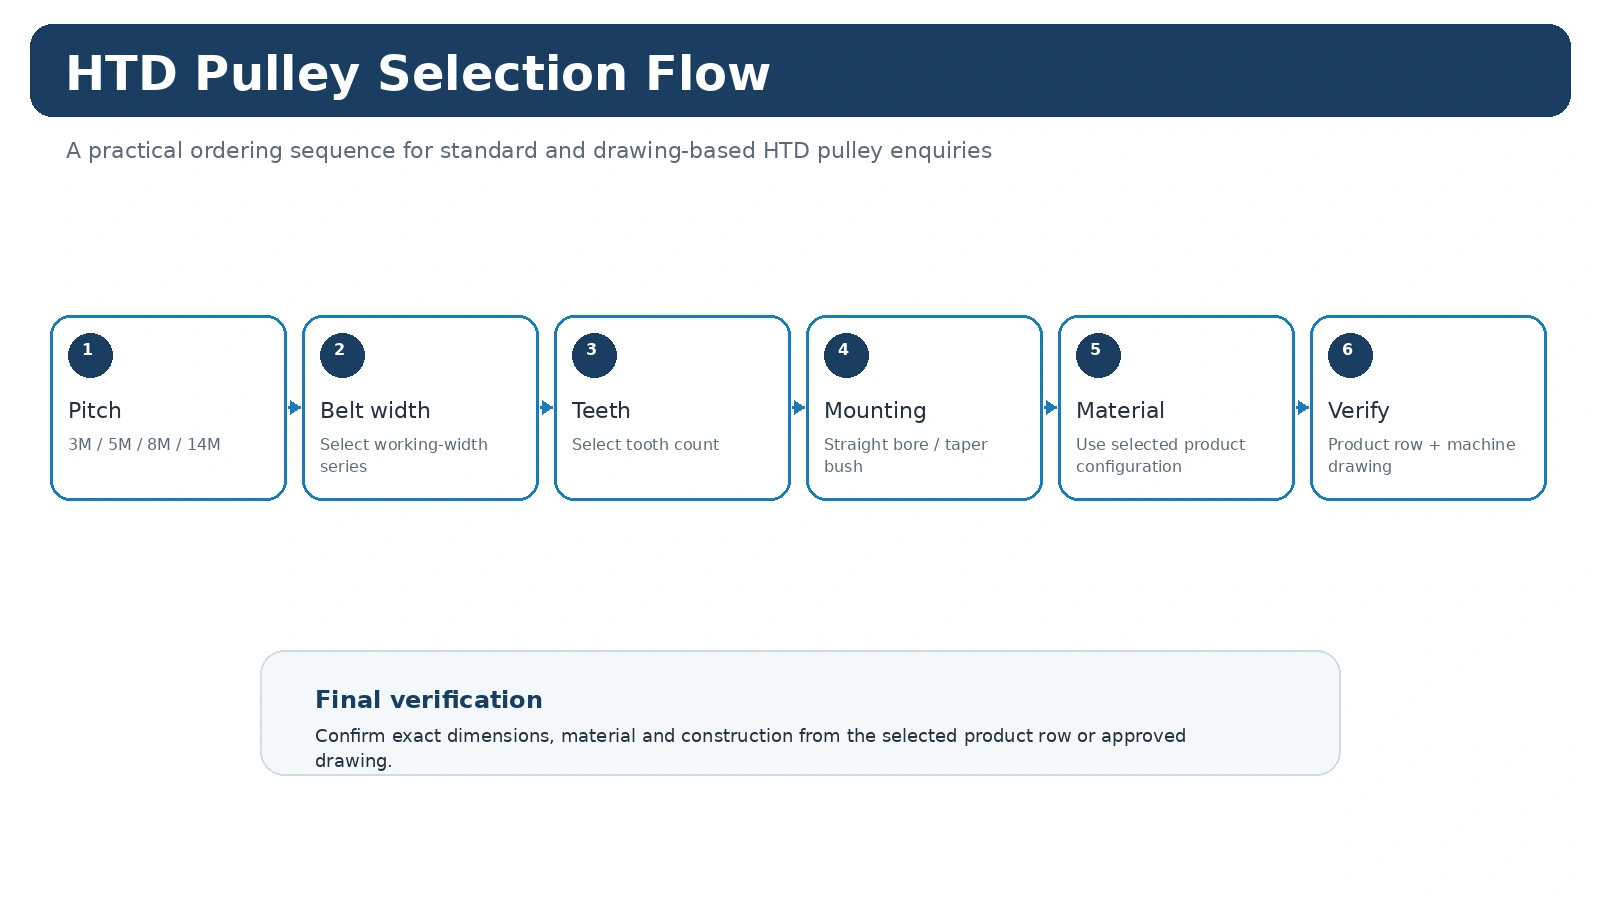
For timing pulley industrial automation, identify the complete belt marking before comparing pulley diameters. HTD is a curvilinear synchronous system and the nominal pitch must stay associated with its profile family. Record the driver and driven tooth counts when an existing ratio must be preserved. For a new drive, document the target speed ratio, driver speed and expected load before choosing tooth counts. This prevents a component-level decision from overriding the machine requirement.
برای یک پروژه تعویض، قبل از تصمیمگیری در مورد معادل بودن یک ردیف کاتالوگ، مقدار اندازهگیری شده را با تسمه نصب شده و چیدمان دستگاه مقایسه کنید. برای یک پروژه جدید، مبنای طراحی را مستند کنید تا تیمهای تعمیر و نگهداری بعدی بتوانند دلیل انتخاب گام، تعداد دندانه و سبک نصب را درک کنند.
ابعادی که نصب را کنترل میکنند
یک قرقره میتواند گام و تعداد دندانهها را مطابقت دهد، اما همچنان به دلیل تفاوت موقعیت سوراخ، توپی، فلنج یا محوری، با دستگاه سازگار نباشد. سطح مشترک شفت، عرض سطح تسمه، برآمدگی توپی در دو طرف و خط تسمه را نسبت به یک مبنای پایدار ماشین اندازهگیری کنید. در جایی که از بوش مخروطی استفاده میشود، هم سری قرقره و هم کد بوش را ثبت کنید. در جایی که سوراخ نهایی مورد نیاز است، تناسب، جای خار و هر روش نگهدارنده را در نقشه لحاظ کنید.
برای یک پروژه تعویض، قبل از تصمیمگیری در مورد معادل بودن یک ردیف کاتالوگ، مقدار اندازهگیری شده را با تسمه نصب شده و چیدمان دستگاه مقایسه کنید. برای یک پروژه جدید، مبنای طراحی را مستند کنید تا تیمهای تعمیر و نگهداری بعدی بتوانند دلیل انتخاب گام، تعداد دندانه و سبک نصب را درک کنند.
شرایط عملیاتی که در انتخاب قرار دارند
The same nominal timing pulley industrial automation component can see very different service depending on the machine. Starts per hour, reversing, shock loading, continuous operating time, temperature, contamination, cleaning and access for tensioning all influence the drive. A compact automation axis emphasizes repeatable motion and controlled alignment, while a conveyor or process machine may emphasize continuous duty and service access. Supply these conditions instead of asking the pulley to be selected from size alone.
برای یک پروژه تعویض، قبل از تصمیمگیری در مورد معادل بودن یک ردیف کاتالوگ، مقدار اندازهگیری شده را با تسمه نصب شده و چیدمان دستگاه مقایسه کنید. برای یک پروژه جدید، مبنای طراحی را مستند کنید تا تیمهای تعمیر و نگهداری بعدی بتوانند دلیل انتخاب گام، تعداد دندانه و سبک نصب را درک کنند.
نکات بازرسی قبل از نصب
بازرسی باید بر ابعادی که بر درایو تأثیر میگذارند تمرکز کند: سطح مشترک شفت، موقعیت محوری، وضعیت دندانه، عرض رویه و هرگونه انحراف یا رابطه مبنا که توسط نقشه کنترل میشود. یک بیانیه کیفیت عمومی، پذیرش را تعریف نمیکند. اگر گزارش ابعادی، سند مواد یا سابقه خاص سفارش مورد نیاز است، قبل از تولید آن را مشخص کنید. در طول نگهداری، مراقب آسیب فلنج، سایش لبه، خرده ریزها و علائمی باشید که نشان میدهد قرقره روی شفت حرکت کرده است.
برای یک پروژه تعویض، قبل از تصمیمگیری در مورد معادل بودن یک ردیف کاتالوگ، مقدار اندازهگیری شده را با تسمه نصب شده و چیدمان دستگاه مقایسه کنید. برای یک پروژه جدید، مبنای طراحی را مستند کنید تا تیمهای تعمیر و نگهداری بعدی بتوانند دلیل انتخاب گام، تعداد دندانه و سبک نصب را درک کنند.
سوالات باز برای بستن قبل از سفارش
چه پروفیل و عرض HTD دقیقی نصب یا مشخص شده است؟
چه نسبت یا تعداد دندانهای موجود باید حفظ شود؟
چه نوع چیدمانی برای سوراخ، اتصال، شیار یا بوش مخروطی مورد نیاز است؟
چه مقدار برآمدگی و فضای آزاد فلنج در توپی وجود دارد؟
سرعت، بار، استارت، دنده عقب و ساعات کارکرد چقدر است؟
کدام نقشهها، مواد یا سوابق بازرسی باید همراه با تحویل کالا باشد؟
چه چیزهایی را باید با RFQ ارسال کرد؟
مشخصات، تعداد دندانه، عرض تسمه، رابط شفت، جزئیات توپی/فلنج، مقدار، مقصد و یک نقشه یا طرح اندازهگیری جایگزین را ارسال کنید. سرعت، نسبت، بار، فاصله مرکز و محیط را برای یک درایو جدید اضافه کنید. بررسی کنید خانوادههای محصولات HTD، استفاده از راهنمای انتخابیا موارد مربوطه را مقایسه کنید یادداشتهای کاربردی.
Automation Drives Need Position and Service Context
For indexing or synchronized motion, record the motion objective, reversal pattern, start-stop frequency and the mechanical elements downstream of the pulley. Repeatability can be affected by belt tension, shaft support and other backlash sources, not only the pulley tooth form.
Capture operating hours, starts and stops, reversal if present, nearby guards and the condition of the shaft support. These details provide the application context for the pulley without turning the page into an unsupported power or life-rating claim.
Replacement Records for Repeated Machine Axes
Plants often have many similar automation axes. Tag the machine position, belt identity and pulley code together so a later maintenance order does not substitute a visually similar pulley from another station.
سابقه خرید باید ارتباط روشنی بین نیاز دستگاه و قرقره انتخاب شده برقرار کند. این بدان معناست که اطلاعات کامل مربوط به مشخصات تسمه یا پروفیل، تعداد دندانه، عرض کاری و رابط شفت به همراه کد محصول باقی میماند. هرگونه ماده خاص، پرداخت، تلرانس کنترلشده، علامتگذاری یا گزارش مورد نیاز باید جداگانه ذکر شود تا با یک ویژگی جهانی کل خانواده اشتباه گرفته نشود.
تدارکات و مستندسازی
پس از مشخص شدن انتخاب، هویت محصول، تعداد، مقصد و اصلاح نقشه پذیرفته شده را در همان خط خرید نگه دارید. قطعات استاندارد کاتالوگ معمولاً بر اساس حداقلهای تعداد تولید برنامهریزی میشوند، در حالی که اقلام بزرگتر یا با ارزش بالاتر را میتوان در برابر ارزش سفارش عملی بررسی کرد. نمونههای واجد شرایط مشتری جدید ۱ تا ۵ قطعهای را میتوان در صورت مناسب بودن پیکربندی و مسیر تولید، با قیمت نمونه بررسی کرد.
سفارشهای مدلهای ترکیبی را میتوان با هم ترکیب کرد و به ارزش عملی حدود ۱۵۰۰ دلار آمریکا رساند. مواد ویژه و فرآیندهای ویژه از حداقل مقدار مورد نیاز آن فرآیند پیروی میکنند. درخواستهای بسیار کوچک یک یا دو قطعهای فقط به عنوان اعتبارسنجی مهندسی واجد شرایط یا نمونههای پولی به جای سفارشهای جایگزین خردهفروشی رسیدگی میشوند.
زمان تحویل پس از مشخص شدن تعریف فنی، تأیید میشود. قطعات استاندارد معمولاً در ۱۰ تا ۲۵ روز کاری، اجزای سفارشی در ۲۰ تا ۴۵ روز کاری و مجموعههای پروژهای یا تجهیزات مرتبط در صورت لزوم در ۴۵ تا ۱۲۰ روز کاری برنامهریزی میشوند. EXW، FOB، CIF و DAP معمولاً پشتیبانی میشوند. FCA، CFR، CPT، CIP و DDP را میتوان برای حمل و نقلهای مناسب مورد بحث قرار داد. این موارد را به عنوان محدودههای برنامهریزی در نظر بگیرید، نه یک وعده حمل و نقل قبل از بررسی سفارش.
یک توالی تصمیمگیری عملی
Start with repeatable motion requirement, ratio, belt family and axis envelope. Keep the machine requirement separate from the catalogue choice: first identify what the drive must preserve, then compare only the rows or drawings that match that identity. This keeps a familiar-looking pulley from being accepted before its functional interfaces have been checked.
For an existing machine, preserve the original relationship before making changes. For a new design, record the target ratio, operating context and installation envelope so the automation-axis selection can be reviewed later without relying on memory or a photograph alone.
ساخت یک رکورد اندازهگیری
The most useful measurement set contains motor speed, driven speed, center distance, pitch family, width and shaft interface. Mark which values were measured on the machine and which values came from a catalogue or released drawing. When a feature is inaccessible, photograph its relationship to a stable datum and identify it as confirmation-required rather than filling the gap with an assumed value.
نقشههای ابعاد باید در عرض کامل و خوانا مشاهده شوند. هرگز یک اسکرینشات را مقیاسبندی نکنید و سپس ابعاد مقیاسبندی شده را به عنوان اندازهگیری در نظر نگیرید؛ از مقدار چاپ شده و نوع ساختار صحیح استفاده کنید.
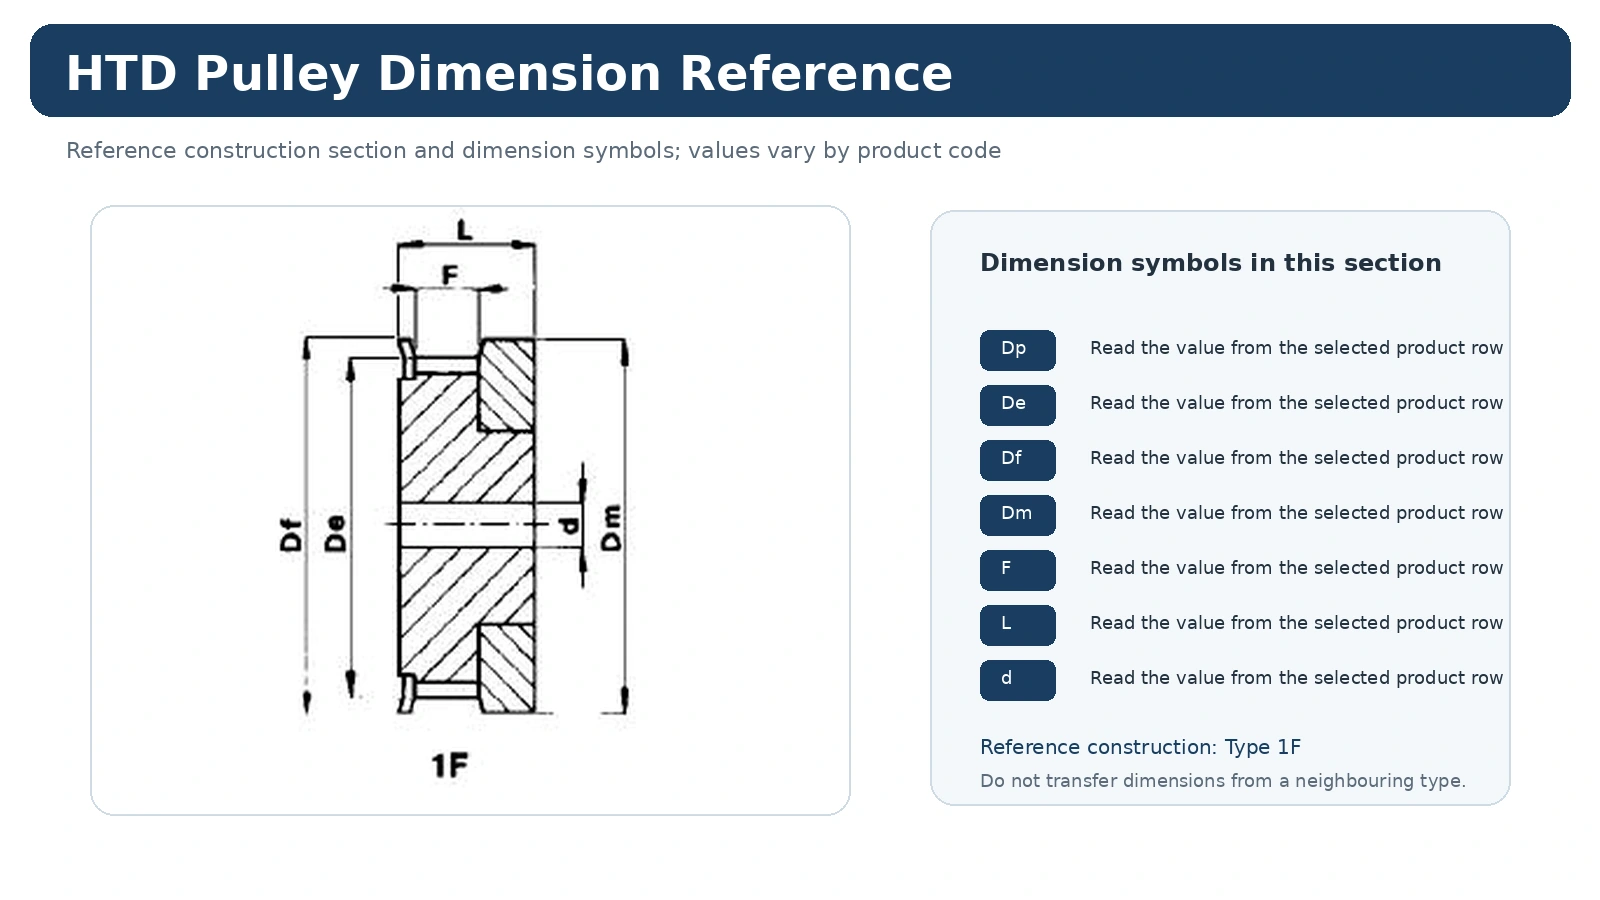
یک حالت شکست که ارزش اجتناب دارد
A common error is selecting a pulley without checking the moving-axis inertia and belt line. That can produce a part that appears close in the catalogue yet changes ratio, belt line, mounting or service access. Resolve the conflicting feature before requesting price so the quotation refers to one mechanically coherent configuration.
اگر دو پیکربندی کاندید همچنان امکانپذیر است، هم اندازهگیریها و عکسهای دستگاه و هم گزینه مورد نظر را ارسال کنید. سپس میتوان با ارائه پیشفاکتور مشخص کرد که کدام رابط هنوز نیاز به تأیید دارد، به جای اینکه عدم قطعیت را به یک مشخصه تبدیل کند.
انتخاب فنی را به یک گزینه آماده برای ارائه پیشنهاد قیمت تبدیل کنید
خانواده HTD/profile و اطلاعات کامل کمربند را بیان کنید.
تعداد دندانه، عرض کار و ابعاد مربوطه یا منابع نقشه را ارائه دهید.
در صورت لزوم، اطلاعات مربوط به سوراخ یا بوش، شفت، برآمدگی توپی و موقعیت تسمه را تعریف کنید.
مقدار، مقصد، مدارک مورد نیاز و نسخه اصلاحشده نقشه مورد استفاده برای درخواست را اضافه کنید.
وقتی یکی از موارد بالا واقعاً ناشناخته است، برای تأیید آن را برچسبگذاری کنید. یک سؤال باز دقیق مفیدتر از یک مقدار محتمل است که هرگز اندازهگیری نشده است.
سوالاتی که خریداران معمولاً میپرسند
اول باید چی تایید بشه؟
Confirm repeatable motion requirement, ratio, belt family and axis envelope. That prevents later dimensions from being compared across the wrong product family or installation route.
چه اطلاعاتی برای جایگزینی مفیدتر است؟
Send motor speed, driven speed, center distance, pitch family, width and shaft interface, plus clear photographs before the old pulley is removed. The photographs preserve axial orientation and neighboring clearances that a loose part cannot show.
چه زمانی باید از نقاشی استفاده کرد؟
هر زمان که ردیف کاتالوگ به طور کامل رابط شفت، چیدمان توپی/فلنج، پرداخت، تلرانس یا الزامات بازرسی مهم برای دستگاه را تعریف نکند، از یک نقشه کنترلشده استفاده کنید.
Machine Conditions to Record for Industrial Automation
Do not select a pulley from the industry name alone. Record the operating pattern of the actual machine: driver and driven speeds or ratio, torque or power where available, center distance, hours per day, start/stop frequency, reversal, contamination and the available guard/shaft envelope. These details explain the duty without turning a general article into an unsupported product rating.
For maintenance replacement, add the installed belt marking, tooth count, working face, hub projection and shaft interface. If there has been edge wear or tracking trouble, capture the belt line and bearing/shaft condition before altering pulley geometry.
Installation Planning for Industrial Automation
Confirm that the selected pulley can be fitted and removed with the available service access. A hub that is technically compatible can still cause downtime if adjacent bearings or guards block installation. Maintain the intended belt plane and review flange clearance so the belt is guided without using persistent flange contact as a substitute for alignment.
Where washdown, dust, fibers, chips or process residue are present, include the environment in the RFQ. Material and maintenance decisions should be reviewed against the actual configuration and environment rather than copied from another application.
Automation Drives Need Repeatable Geometry More Than Generic “High Precision” Claims
Automation equipment often depends on repeatable position relationships between a motor, driven axis and feedback or indexing sequence. The useful pulley specification is therefore the one that preserves the intended ratio, belt family, axial belt line and shaft connection. A general claim of precision does not replace those measurable interfaces.
Before ordering a replacement, record the tooth counts on both pulleys when possible, the belt marking, center distance and the axial position of the working face. Check whether the pulley is mounted directly on a motor shaft, intermediate shaft or gearbox output because available hub length and removal access can differ. Photograph sensor targets, couplings or guards that share the same shaft envelope.
For a new automation axis, add acceleration pattern, reversals and duty information to the RFQ without assuming a universal rating from the pulley page. That gives the belt-system review the machine context it needs while keeping the published product data tied to the actual catalogue geometry.
Keep the Pulley Change Visible to the Controls and Maintenance Teams
If the pulley tooth count is changed intentionally, document the change with the machine team because the speed relationship and any motion or timing assumptions may also change. A replacement intended to restore the original machine should normally preserve the identified tooth-count pair and belt family instead of using the nearest available diameter.
After installation, inspect the belt path through the machine’s normal safe commissioning process. If an axis exhibits new edge contact, noise or visible tracking movement, stop and recheck the belt line, shaft interface and spacer arrangement before treating the symptom as a belt-quality issue.
Define the Motion Requirement Before the Pulley Model
Automation drives can include indexing, positioning, transfer and auxiliary axes with different motion profiles. The pulley selection therefore starts with the machine function, required ratio, belt system, center distance and installation envelope. The product page then supplies the catalogue geometry needed to connect that drive decision to a real pulley configuration.
Repeated reversing or positioning duty can make alignment, shaft support and mounting security more important to investigate, but the website does not assign a universal precision or torque rating to every pulley. If the axis has a controlled positioning, runout or repeatability requirement, place that requirement on the machine or component drawing and describe the measurement method.
State indexing, positioning, transfer or continuous drive duty.
Provide ratio, center distance, belt family and available pulley envelope.
Record shaft diameter, bore or bush and axial belt-line position.
Include guarding, contamination, temperature or access constraints that affect the installation.
For a retrofit, photograph the original drive before changing pulley diameter or tooth count. A ratio change alters machine motion as well as component size, so the automation logic and mechanical layout should be reviewed together.